Buyer's Guide to Tooling Materials for High-Volume Stamping
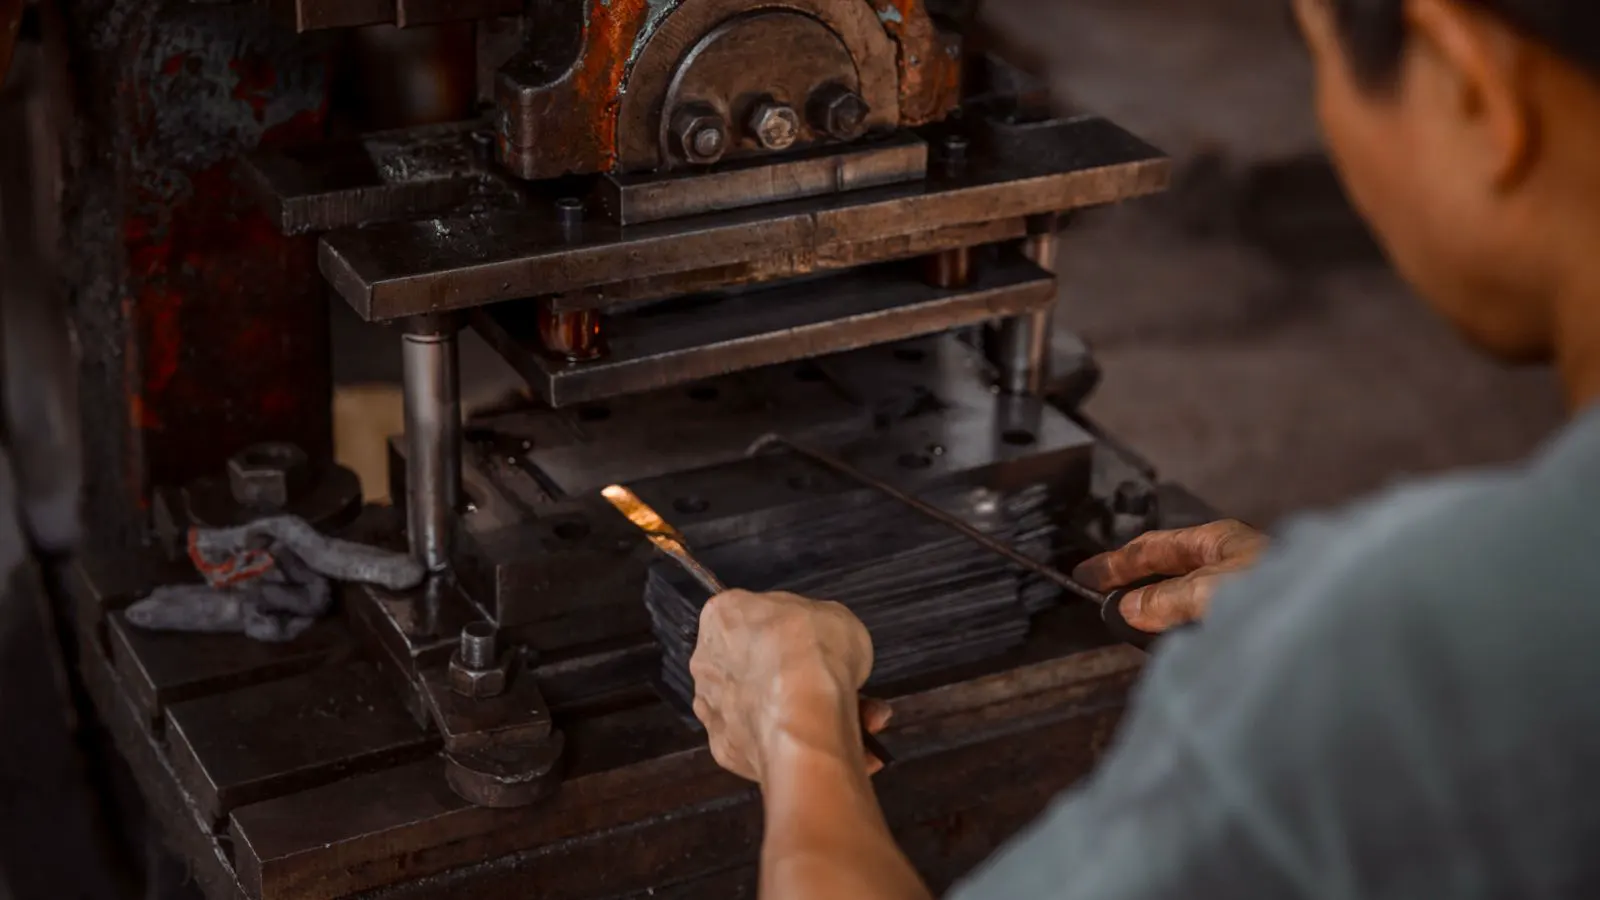
Die material choice directly impacts tooling costs and production life. This guide explains how to evaluate hardness, toughness, and wear resistance to minimize total cost ownership for high-volume stamping jobs.
- Match die steel hardness and toughness to the expected production volume and part geometry.
- Evaluate total cost ownership by combining tooling cost, expected life, maintenance, and scrap rates.
- Use a criteria table to compare materials before committing to a tooling supplier.
- Shorter lead times for tooling can offset higher material costs when production start dates are tight.
- Revisit material choices when part design, tolerances, or production volumes change significantly.
Why Die Material Drives Total Cost Ownership
The first cost of a stamping die is not the material. It is the combination of material, grinding, heat treatment, and labor that creates the tooling. A high hardness die may cost more to build but run longer before a rebuild. A softer tooling material may reduce the initial invoice and still fail early under heavy production loads.
Total cost ownership measures the full expense of a die over its active life. It includes the purchase price, expected production life, maintenance, and the cost of scrap or downtime when the tooling wears. For high-volume stamping, the difference between materials can shift the winner of a bid. A slightly cheaper die that needs replacement twice a year will usually cost more than a premium tool that lasts several times longer.
The material must also match the part. Thin sheet metal may need a different edge than a heavy structural section. A part with sharp corners will wear a punch differently than a flat blank. The tooling supplier should be able to point to the specific features that drive material selection.
How Die Steel Selection Affects Upfront Cost
Die steel selection changes the tooling budget in several ways. Harder steels are more expensive to source and harder to machine. They often require slower cutting speeds and more frequent tool changes during the build. The heat treatment process adds time and energy. A die built with a standard carbon tooling steel may be ready sooner than one made from a high alloy steel.
The supplier’s labor rates and shop capacity also influence the final price. A shop with deep heat treating capability may charge differently than one that outsources that step. The tooling price is not just a material cost. It reflects the total work required to make the die perform at the expected life.
Lead time is part of the upfront cost. If a production line is waiting for parts, the cost of a longer tooling build is higher than the sticker price. A faster build may justify a higher material grade. The buyer should ask the supplier to break down the tooling cost into material, labor, heat treating, and finishing. This breakdown makes it easier to compare quotes and understand where the money is going.
How Durability Changes Long Term Cost
The life of the die is measured in parts produced. Each punch, die block, and forming surface wears over time. A die that produces a million parts before a rebuild has a much lower per part cost than one that fails at two hundred thousand. The material determines how fast those surfaces wear.
Wear is not always the same across the die. Cutting edges wear faster than flat forming surfaces. A punch that shears a thick plate will wear differently than a punch that forms a shallow bend. The material must handle the specific stress of the job. A hard material may chip if the press load is uneven or if the part geometry is aggressive.
Maintenance cost also falls into this category. A die that needs frequent sharpening or rework adds labor hours to the production schedule. Each rebuild takes the press offline. The cost of that downtime depends on the value of the production line and the urgency of the part. A high volume die with a short life can create a constant cycle of maintenance that erodes the savings from a low upfront tooling cost.
A Practical Criteria Table for Material Choice
The table below lists the main factors to weigh when comparing die materials. Use it during the review of tooling quotes and when discussing material options with the supplier.
| Criterion | What to look for | Why it matters |
|---|---|---|
| Hardness | Match to part thickness and edge geometry | Harder material resists wear but may chip under high stress |
| Toughness | Ability to absorb shock and uneven loads | Prevents cracking and extends tool life under variable conditions |
| Thermal stability | Consistency after heat treating | Ensures the die holds its dimensions over long production runs |
| Machinability | Ease of grinding and finishing | Affects tooling cost and build lead time |
| Expected life | Parts per rebuild based on material | Directly impacts the total cost per part over the run |
| Maintenance profile | Frequency of sharpening and rework | Affects downtime and labor costs during production |
This table is a starting point. The supplier should be able to explain how the specific material choice supports each row. If a quote lists a material without explaining the expected life, ask for a breakdown of the wear factors. The supplier should be able to point to the part features that drive the selection.
How to Evaluate a Tooling Supplier’s Material Recommendation
A good supplier will not just list a material. They will explain why it fits the part. Ask for the expected life in parts. Ask for the heat treating specification. Ask what happens when the die reaches its end of life and whether a rebuild is possible or if a new tool is required.
Check the supplier’s history with similar parts. If they have stamped a high volume run of a similar thickness and geometry, they can point to the material they used and the results. If they have no experience with a similar part, they should be transparent about the risk. The buyer can then decide whether to accept a shorter trial life or require a more conservative material choice.
The supplier should also provide a maintenance schedule. This document should list the expected number of parts before each component needs inspection or sharpening. It should include the cost of those services. This information helps the buyer build a realistic total cost ownership model. Without it, the tooling quote is only half the story.
Building a Total Cost Ownership Model
The total cost ownership model starts with the tooling cost. Add the expected production life in parts. Divide the tooling cost by the expected life to get the tooling cost per part. Then add the cost of maintenance, rebuilds, and scrap. Compare this number across different material choices.
The model should account for the press capacity. A high speed press produces more parts per hour, which increases the wear rate. A low speed press may extend the tool life but costs more in labor and energy. The production plan should be part of the material selection process.
The buyer should also consider the risk of failure. A die that fails early can cause a production stoppage. The cost of that stoppage may outweigh the savings from a cheaper material. A conservative material choice that extends life by a few months may be worth the extra upfront cost. The goal is to balance the initial invoice against the long term cost per part.
A Decision Checklist for High Volume Stamping
Use this checklist when reviewing a tooling proposal for a high volume run.
- The material choice is explained with reference to the part thickness and geometry.
- The expected life in parts is provided for each major die component.
- The heat treating specification is included in the quote.
- The tooling cost is broken down into material, labor, and finishing.
- A maintenance schedule with rebuild intervals is provided.
- The lead time for the tooling build is confirmed in writing.
- The supplier has experience with a similar part or process.
- The total cost per part is calculated using the expected life.
- The press speed and production volume are part of the analysis.
- The end of life plan is defined, including rebuild options.
This checklist ensures that the material selection is not just a technical choice. It is a business decision that balances cost, risk, and production needs. The buyer should use the information to make an informed choice and to hold the supplier accountable for the expected performance.
When to Revisit the Material Choice
The material choice is not permanent. If the part design changes, the material may need to change. If the production volume increases, the tooling may need to be upgraded. If the current material is causing excessive scrap or downtime, a different steel may be better.
The buyer should track the actual life of the die against the expected life. If the die fails early, the supplier should be involved in the root cause analysis. The issue may be the material, the press setup, or the part design. The data from the actual run will guide the next tooling decision.
A long term relationship with the tooling supplier makes this review easier. The supplier can track the die performance over time and suggest improvements. The buyer can use the data to refine the material choice for future runs. This process reduces risk and improves the total cost ownership over the life of the part.
Final Thoughts
Die material selection is a key factor in the total cost ownership of a high volume stamping die. The upfront cost of the tooling is only part of the picture. The expected life, maintenance, and downtime cost are often larger factors. A careful evaluation of the material against the part requirements and production plan will lead to a better decision.
The buyer should ask for a breakdown of the tooling cost and a clear explanation of the expected life. The supplier should be able to provide a maintenance schedule and a rebuild plan. With this information, the buyer can compare material choices and make a decision that balances cost and performance.
The goal is not to pick the cheapest tooling. The goal is to pick the tooling that delivers the lowest total cost per part over the life of the run. The material choice is the starting point for that decision.
Frequently asked questions
How do I know if a cheaper die material will save money?
Calculate the tooling cost per part by dividing the tooling cost by the expected life in parts. Add the cost of maintenance and downtime. If the cheaper material requires more frequent rebuilds, the total cost per part will be higher.
What is the difference between tooling cost and total cost ownership?
Tooling cost is the price of the die. Total cost ownership includes the tooling cost plus the cost of maintenance, rebuilds, scrap, and downtime over the life of the die.
Should I always choose the hardest die steel available?
No. The hardest steel may be more expensive to machine and heat treat. It may also chip if the part geometry or press load is too aggressive. The material must match the specific requirements of the part and the production environment.
How does press speed affect die material selection?
Higher press speed increases the wear rate of the die. A material that lasts a long time at a low speed may fail quickly at a high speed. The production plan should be considered when choosing the material.
What should I do if a die fails earlier than expected?
Work with the supplier to perform a root cause analysis. Check the material, the press setup, and the part design. Use the data to adjust the material choice or the maintenance schedule for future runs.