Checklist: 6 Questions for Stamping Supplier Capabilities
This checklist provides six direct questions to verify a stamping vendor's capabilities. It helps buyers confirm production capacity, quality systems, and tooling ownership before awarding work, reducing the risk of late deliveries and quality failures.
- Ask directly about press tonnage, number of stations, and tooling ownership to verify physical capacity.
- Request audit reports, PPAP documentation, and traceability records to confirm quality control.
- Evaluate communication protocols and change management to ensure design changes do not halt production.
- Confirm material sourcing and inspection standards to prevent defects in final parts.
- Use this checklist during vendor selection to reduce the risk of supply chain disruptions.
1. Can the Supplier Confirm Specific Press Tonnage and Tooling Ownership?
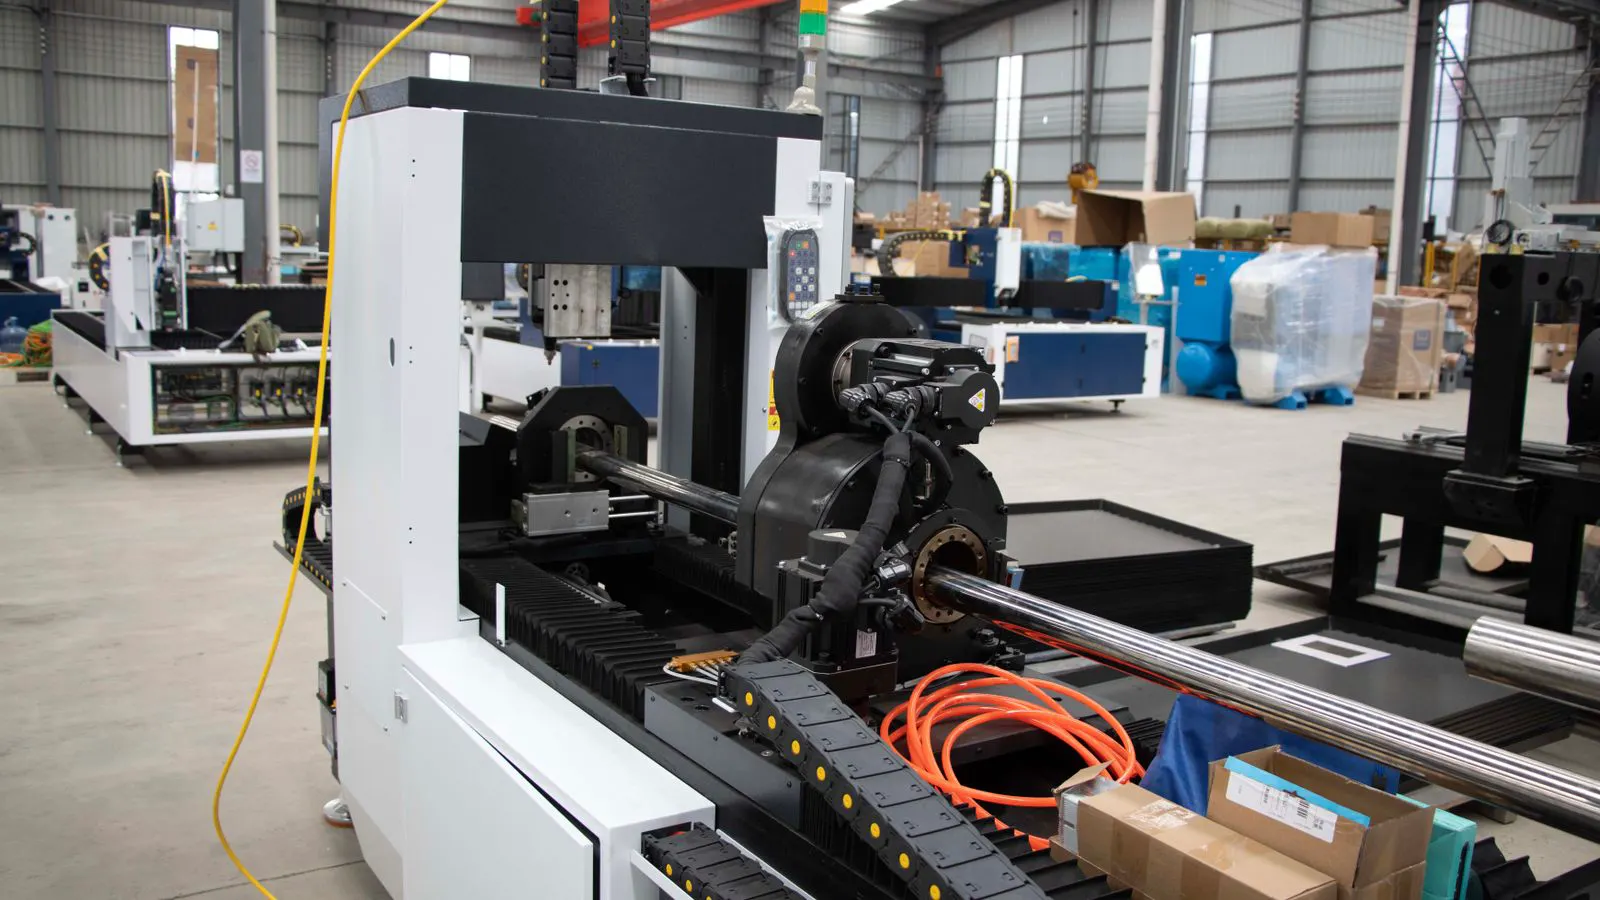
The first question to ask a stamping vendor is whether they can confirm specific press tonnage and tooling ownership. Many buyers skip this step, assuming that a company with a large factory floor can handle any part. That assumption rarely holds. A large facility does not mean it has a 1,000-ton progressive die press. It may only have a 100-ton hydraulic press and a few mechanical presses.
Start by asking for a list of installed presses. Request the make, model, and tonnage rating for each machine. Then ask which press will run the specific part. This detail matters because different parts require different forces. A deep draw part in 18-gauge steel may need a different tonnage than a flat blank. A complex progressive die may need a different die set than a simple punch-and-die tool.
Tooling ownership is the second half of this question. Ask who owns the dies. If the supplier owns the dies, they hold the production data. If the buyer owns the dies, the supplier must provide strict change control. This distinction affects lead times and cost. If the buyer owns the dies, the supplier may charge a holding fee or require a deposit. If the supplier owns the dies, the buyer may face higher per-unit costs but lower upfront risk.
Red flags to watch for include:
- The supplier cannot name the specific press that will run the part.
- The supplier claims to have “high tonnage” but refuses to list the exact machine.
- The supplier does not know if they own the dies or if the buyer does.
- The supplier says the dies are “in-house” but cannot show the tooling inventory.
2. What Is the Actual Production Capacity for This Specific Part?
The second question asks about actual production capacity for the specific part, not general factory output. A supplier may claim to stamp 10 million parts per month in total. That number includes every product they make. It does not tell you if they can make 500,000 of your part per week.
Ask for a capacity calculation. This should include the number of parts per die strike, the number of strikes per hour, the number of shifts, and the number of days per week. Then ask about changeover time. If the part requires a new die setup, how long does it take to change from the previous part? If the changeover is four hours and the part runs for 30 minutes per cycle, the effective capacity drops significantly.
Request a written capacity statement. This document should show the math, not just a number. A good supplier will break down the calculation. They will show the die strike rate, the number of good parts per strike, and the downtime allowance. If the supplier gives a single number without a breakdown, treat it as a guess.
Red flags to watch for include:
- The supplier provides a monthly number but cannot break it down by shift.
- The supplier assumes a 24-hour operation without confirming shift schedules.
- The supplier does not account for die changeover time.
- The supplier gives a capacity that is exactly double the requested order size without explaining why.
3. How Does the Supplier Control Quality and Traceability?
The third question focuses on quality control and traceability. Metal stamping is a high-speed process. Defects can appear in a single minute and affect thousands of parts. You need to know how the supplier catches them before the parts leave the building.
Ask for a quality plan. This should include in-process checks, final inspection methods, and acceptance criteria. Request examples of Control Plans and PPAP documents. A PPAP document shows how the supplier proved the process was capable before mass production. It includes gauge R&R studies, process capability studies, and material certifications. If the supplier has not done a PPAP, ask when they plan to do one.
Traceability is the second part of this question. Ask how the supplier tracks material lots, heat numbers, and die numbers. If a defect appears in a customer part, the supplier must be able to trace it back to the specific die strike, the specific material lot, and the specific operator. Request a sample traceability record. This is usually a simple table showing part number, die number, material heat number, date, and quantity.
Red flags to watch for include:
- The supplier only inspects finished parts and does not inspect in-process.
- The supplier cannot show a sample Control Plan or PPAP.
- The supplier does not track material heat numbers.
- The supplier says “we inspect everything” but cannot explain the method.
4. What Is the Supplier’s Material Sourcing and Inspection Process?
The fourth question asks about material sourcing and inspection. Material quality is a common source of stamping defects. If the material has a hidden defect, the press may not catch it. The part will look fine, but it will fail in service.
Ask who supplies the raw material. If the supplier buys from a third party, ask for a list of approved material suppliers. Request mill certificates. A mill certificate shows the chemical composition, mechanical properties, and heat number of the material. Without this document, you cannot verify that the material meets your specification.
Ask about incoming inspection. Does the supplier inspect material before it goes to the press? If so, what do they check? They should check thickness, hardness, and visual condition. If they do not inspect material, ask why. Some suppliers trust the mill. That is a risk you may not want to take.
Red flags to watch for include:
- The supplier cannot provide mill certificates for recent shipments.
- The supplier buys material from multiple sources without approval from you.
- The supplier does not inspect material before stamping.
- The supplier says “the material is from a known supplier” but cannot name them.
5. How Does the Supplier Manage Design Changes and NCRs?
The fifth question is about change management. Design changes are inevitable. A customer may change a hole size, add a bend, or change the material grade. You need to know how the supplier handles these changes.
Ask for a change control process. This should include a written request, a review of the change, a cost impact, and a schedule update. The supplier should not make a change without your written approval. If they do, you have a liability.
Ask about the Non-Conformance Report (NCR) process. If the supplier finds a defect, how do they report it? They should send you an NCR before shipping the affected parts. The NCR should include the description of the defect, the quantity affected, the root cause, and the corrective action. If the supplier ships defective parts and then reports the NCR, you have a problem.
Red flags to watch for include:
- The supplier makes changes without written approval.
- The supplier does not have a written change control process.
- The supplier reports NCRs only after shipping.
- The supplier does not track the closure of NCRs.
6. What Communication and Escalation Protocols Are in Place?
The sixth question asks about communication. Stamping is a physical process. Problems happen. A die breaks. A press fails. A material lot is rejected. You need to know how the supplier will communicate these events.
Ask for a point of contact. This should be a person who can answer questions quickly. Ask for their name, title, and direct phone number. Do not accept a general email address. Ask about escalation. If the point of contact is unavailable, who is the next person? What is the escalation path?
Ask about reporting. How often will the supplier send production reports? Daily? Weekly? What should the report include? It should include quantity produced, scrap rate, and any quality issues. A good supplier will send a report even if everything is normal. A bad supplier will only send a report when something goes wrong.
Red flags to watch for include:
- The supplier does not have a designated point of contact.
- The supplier does not provide a direct phone number.
- The supplier does not have a reporting schedule.
- The supplier only communicates by email and does not answer phone calls.
7. How Should You Document and Validate These Answers?
The final step is to document the answers. Do not rely on a verbal conversation. Ask the supplier to send a written response to each question. This becomes part of your due diligence file.
Create a supplier scorecard. Rate each answer from 1 to 5. A 5 means the answer is clear, specific, and supported by evidence. A 1 means the answer is vague, missing, or contradictory. Use this scorecard to compare multiple suppliers.
Remember that supplier capabilities are not static. A supplier that was strong in 2023 may be weak today. A new press may be under maintenance. A key engineer may have left. Revisit this checklist annually. Update it if the supplier changes their facility, their management, or their quality system.
This checklist is not a replacement for a site audit. It is a filter. It helps you identify serious gaps before you spend money on a travel audit. If a supplier fails three or more of these questions, do not proceed. The risk is too high.
Frequently asked questions
Do I need to audit every supplier using this checklist?
No, you need to use this checklist for every new supplier. You can use it as a filter before a full site audit. If a supplier fails basic questions, do not travel.
What if the supplier cannot provide a PPAP document?
Ask them to create one. A PPAP is a standard industry document. If they refuse, it suggests they do not have a mature quality system.
Can I use this checklist for low-volume stamping?
Yes. The questions apply to any stamping volume. Low-volume parts often have higher tooling risk, so capacity and tooling ownership are even more important.
How often should I review supplier capabilities?
Review them at least once a year. Also review them after any major change in the supplier, such as a new manager, a new press, or a quality incident.
What if the supplier says they "will figure it out" for a missing document?
Do not accept that answer. A professional supplier should have the document or a clear plan to create it. "We will figure it out" is a red flag for poor process control.