Outlook: AI Inspection in Stamping QC
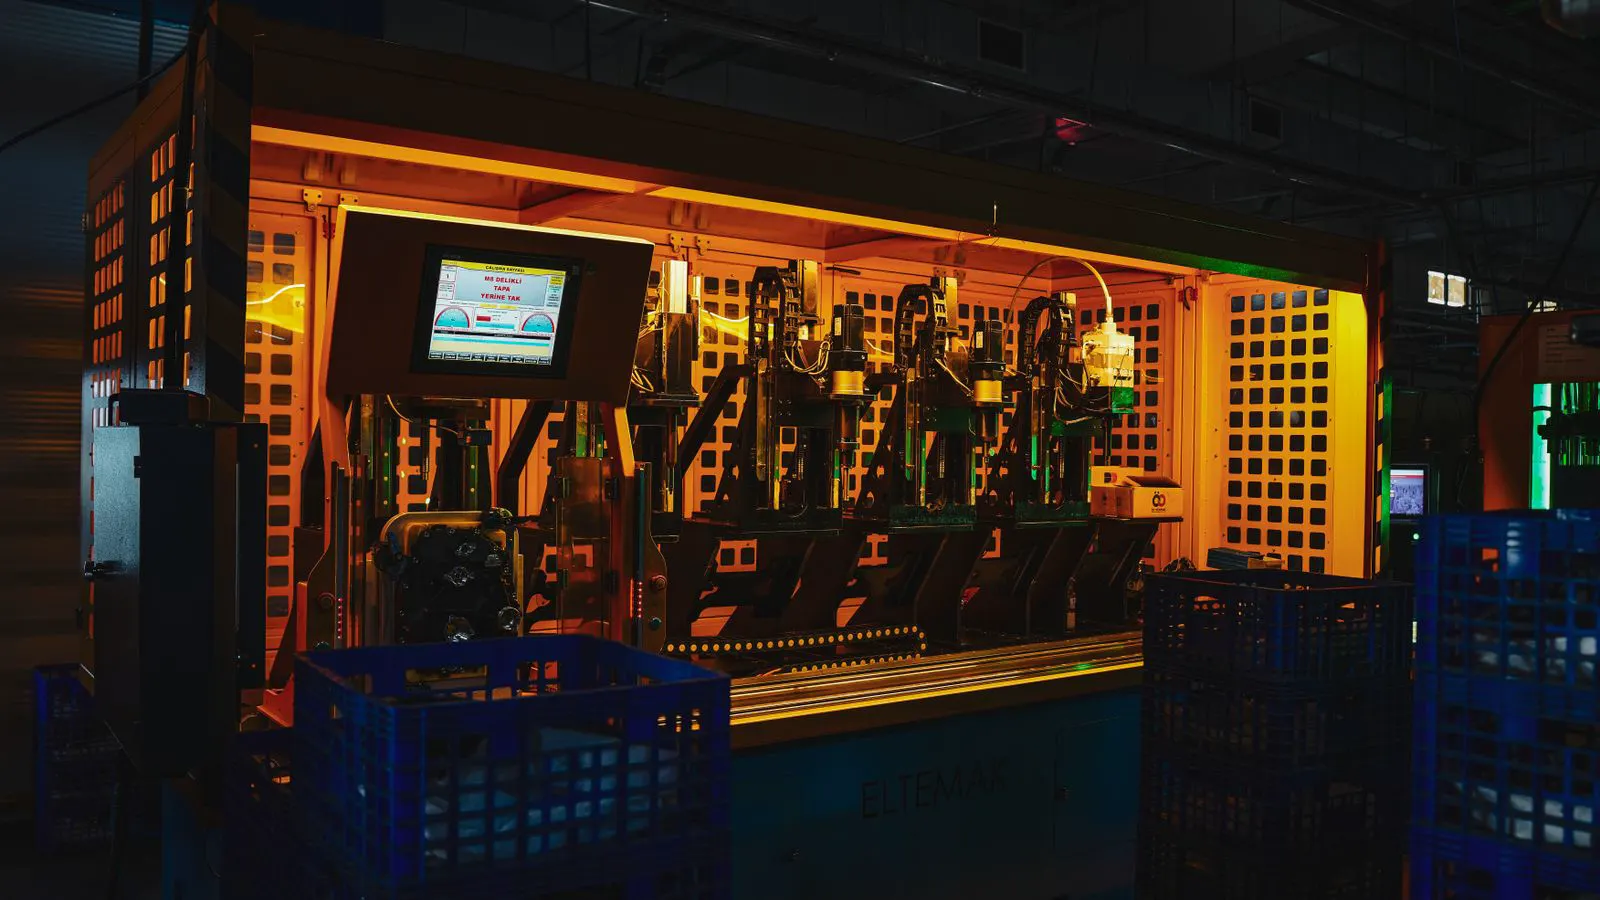
AI inspection is shifting metal stamping quality control from manual sampling to continuous, data-driven monitoring. Leaders should prepare for changes in defect detection, documentation, and process feedback loops. This outlook covers five shifts and practical steps for your team.
- AI inspection reduces reliance on manual gauging by capturing data continuously.
- Visual defect detection improves consistency compared to spot checks.
- Integrated data feeds enable faster feedback loops to the stamping operator.
- Preparation requires updating SOPs and training staff on new inspection roles.
- Buyers should verify data output formats and integration capabilities with their ERP or MES.
Where AI inspection fits in the current workflow
Most stamping shops already use some form of visual inspection. Operators check first parts, sample finished parts, and review scrap piles. AI inspection changes the frequency and depth of that work. Instead of checking every tenth part with a caliper or a CMM, a vision system watches every part as it leaves the die.
This shift does not replace the press, the die, or the engineer. It changes who inspects and how often. The machine sees. The human decides. The data is recorded automatically.
The result is a tighter feedback loop. When a burr appears on a flange or a punch marks show up on a thin sheet, the system flags it in real time. The operator can stop the line before a full batch is rejected.
Shift one: from sampling to continuous monitoring
Traditional quality control relies on sampling. You pick ten parts per hour. You check the critical dimensions. If those ten pass, the hour is green. If one fails, you hold the batch and investigate.
AI inspection removes the sampling gap. A camera captures every part. The software compares the image against the approved standard. It checks for scratches, dents, paint spots, missing features, and out-of-tolerance shapes.
This works best when the defect is visible. Surface finish issues and small dimensional variances are easier to detect than hidden internal defects or material hardness changes. For those, you still need physical gauges or lab testing.
The practical change is in your SOPs. You no longer define “sample size” for surface checks. You define “coverage.” Every part is inspected. Your quality plan updates to reflect 100% visual coverage instead of AQL sampling.
Shift two: from subjective judgment to defined thresholds
A human inspector has limits. Lighting changes. Fatigue sets in. One person calls a scratch acceptable. Another rejects it. AI removes that variability. You set a threshold. The software applies it uniformly.
This is where the specification work matters. If you want the system to catch a 0.5 mm burr, you must define what a 0.5 mm burr looks like. You provide reference images of good and bad parts. You tune the sensitivity.
The trade-off is setup time. A generic vision system may miss subtle defects that only a trained eye catches. A tuned system will flag every part against your standard. You must invest in the tuning phase, or the system will either miss real defects or create noise with false positives.
For buyers, ask for sample data from similar parts. Do not trust the vendor demo alone. Test your actual product against their system before committing to a purchase.
Shift three: from paper records to digital audit trails
Every manual inspection generates a paper log or an entry in a spreadsheet. You record the part number, the date, the operator, and the result. When an audit comes, you hunt through those records.
AI inspection generates a digital trail automatically. Each part has a timestamped image, a pass/fail result, and a link to the specific die and shift. If a customer complaint arrives six months later, you pull up the exact image of the suspect lot in seconds.
This changes how you handle PPAP and APQP documentation. The inspection data becomes part of the quality record. You can export it in CSV, PDF, or API format to match your ERP or MES.
The risk here is data management. If you inspect thousands of parts per hour, the image storage grows fast. You need a plan for archiving, retention, and access. Do not let the camera become a black box. Ensure the data is searchable and retrievable by part number, date, and defect type.
Shift four: from detection to prevention
The biggest value of AI inspection is not catching bad parts. It is predicting them. When the system sees a trend, it can alert the operator before the defect becomes a batch reject.
For example, if the software detects a slight increase in burr size over 50 parts, it may alert you to a worn punch edge. If it sees a pattern of minor dents, it may point to a pressure drop in the ram. The operator can intervene early.
This requires the system to be connected to the process, not just the result. It needs to log the press parameters, the tooling ID, and the material batch. When a defect appears, the data tells you what changed.
You do not need a full machine learning platform to get this benefit. Even simple threshold alerts are useful. If the defect rate crosses a set limit, the system flags the shift. The operator investigates. The root cause is addressed before the next batch.
Shift five: from standalone checks to integrated quality
AI inspection works best when it is part of a larger quality ecosystem. It does not sit alone on the line. It feeds into your quality management system. It triggers corrective actions. It updates the die maintenance schedule.
If the system detects a recurring defect, it should generate a work order. If a die tool wears beyond a threshold, it should flag it for replacement. If a material lot causes high rejection, it should alert the buyer.
This integration changes the role of the quality engineer. You spend less time pulling data from spreadsheets and more time analyzing trends. You can look at defect rates by shift, by operator, by die, and by material supplier.
For buyers, this is where you ask about integration. Can the camera output data to your existing MES? Can it trigger an automated stop? Can it export reports in a format your compliance team accepts? If the answer is no, you will end up with a siloed system that requires manual re-entry.
How to prepare your team and process
The transition to AI inspection is not just a hardware purchase. It is a workflow change. Your team needs to understand what the system does and what it does not do.
First, update your SOPs. Define who operates the camera, who reviews flagged parts, and how false positives are handled. The operator still has the final say on a part. The system gives them information.
Second, train your inspectors. They will no longer do 100% visual checks by hand. Their role shifts to reviewing AI flags, tuning thresholds, and investigating root causes. This requires different skills.
Third, review your drawing specifications. If your drawing does not define surface finish or defect acceptance, the AI system has no standard to follow. You must specify what “good” looks like. Include reference images if possible.
Fourth, plan for the data. Decide where the images are stored. How long do you keep them? Who has access? This is a compliance issue as well as a technical one.
Fifth, start small. Do not buy a full line of cameras for every press. Pick one high-value part or one critical defect type. Test the system. Measure the time saved. Measure the reduction in escapes. Then scale.
What to ask vendors before buying
When you talk to an AI inspection vendor, focus on practical integration. Do not get distracted by flashy demos.
Ask how the system handles lighting changes. Stamping shops have moving parts, shiny metal, and varying ambient light. If the camera struggles with glare, your inspection will be inconsistent.
Ask about false positive rates. A system that flags 20% of good parts will frustrate your operators. They will start ignoring the alerts. You need a system that is accurate enough to trust.
Ask about the training process. Who tunes the system? How long does it take? Do you need to send parts to their lab, or can they train on-site?
Ask about support. When the system fails, who responds? How fast? You cannot afford downtime for a camera that stops inspecting.
Ask about the output. Can you export the data in a format your quality team uses? Can you generate reports for customer audits? If not, you will spend hours converting files.
The role of the human inspector does not disappear
AI inspection does not make your quality team redundant. It changes their focus. The human inspector still handles complex parts that are hard to automate. They still perform first article inspections with physical gauges. They still investigate root causes when the AI flags a trend.
The value is in the shift from repetitive checking to analytical work. Your team spends less time measuring the same dimension on every part and more time solving why the dimension is drifting.
This is the future of quality control in metal stamping. It is not about replacing people with machines. It is about giving people better data so they can make better decisions.
Prepare your process. Define your standards. Test the technology. And keep your focus on the part, not the tool.
Frequently asked questions
Does AI inspection replace manual gauging?
No. It complements it. AI is best for visible surface defects and consistent dimensional checks. Manual gauging remains necessary for complex shapes, material properties, and first article verification.
How long does it take to set up an AI inspection system?
Setup time varies by part complexity and lighting conditions. A simple part with clear defects may take a few days. A complex part with subtle surface issues may take several weeks of tuning.
Can AI inspection handle shiny metal surfaces?
Yes, but it requires proper lighting and camera setup. Specular reflections can confuse the software if the lighting is not controlled. Vendors with experience in metal stamping will have solutions for this.
What data output formats are standard?
CSV, PDF, and API integration are common. Some systems also support native integration with MES or ERP platforms. Confirm the output format matches your internal systems before purchasing.
How do I handle false positives from the AI system?
Establish a review process. When the system flags a part, the operator makes the final decision. Track false positives over time. If the rate is high, retune the thresholds. Do not ignore the flags, but do not let them stop the line unnecessarily.


